Printers
Printer Comparison Table
| Printer Type | Materials | Layer Height (mm) | Support Style | Build Volume (in) |
|---|---|---|---|---|
| Formlabs 3 & 4 LFSLA/MSLA 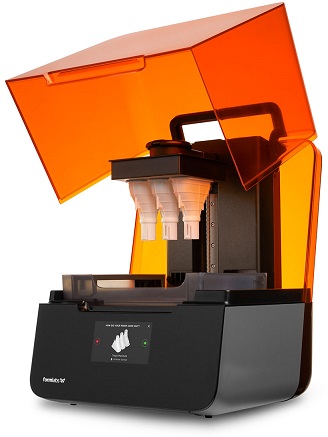  |
Photopolymer Resin – Stock: Clear, Tough 2000, Durable, Flexible (Legacy V2 80A), Elastic (V1 50A), Rigid 4000, High Temp, Castable. Materials Guide. |
0.025 – 0.3 (0.1 default) | Breakoff | 5.7 x 5.7 x 6.9 (height) |
| Bambu Lab X1C, P1S and P2S FFF*   |
Thermoplastic Filament 0.4mm nozzle: PLA, PETG, TPU for AMS (68D) 0.6mm Nozzle: TPU 95A, TPU 90A, TPU 85A, PETG-CF, PLA-CF Materials Guide. |
0.08 – 0.42 (depending on nozzle size, default is 0.2-0.3) | Breakoff standard, Dissolvable is an option for select materials | 9.25 x 9.8 x 9.8 (height), exclusion zone in one corner 0.71 x 1.10 |
| Bambu Lab H2D FFF* |
Thermoplastic Filament 0.4mm nozzle: PLA, PETG, ABS, PC, ASA Aero, PLA Aero, PA, ASA, TPU for AMS (68D) 0.6mm Nozzle: TPU 95A, PETG-CF, PLA-CF Materials Guide. |
0.08 – 0.42 (depending on nozzle size, default is 0.2-0.3) | Breakoff standard, Dissolvable is an option for select materials | 11.8 x 12.55 x 12.55 (height) |
**Stock updated 10/14/2026
Formlabs Printers
We have two models of printers from Formlabs at EPIC. The Form3 is a LFSLA, which stands for Low Force Stereolithography that uses a LPU or light processing unit to move back and forth under the tank and cure each layer of the print. The Form4 is a MSLA, which stands for Masked Stereolithography, this operates differently and it cures each layer all at once and does not have any moving parts. The “Masked” part refers to an LCD that is used to block the UV where you do not want the resin to cure in each layer printed. For more information on how each technology works visit the Formlabs blog on the topic. The layer height ranges from 0.025mm to 0.30mm and the selection available will vary with the type of resin you are printing with. For most prints 0.1mm layer height is a good balance between surface smoothness and print time so this is our default for prints. For further details on each resin available from Formlabs please visit their Resin Selector website. The resins we currently stock are listed in the table above. If you wish to use a resin which we do not stock please contact us, you may have the option to purchase the resin and resin tank and provide them to EPIC to complete your print requests. Form2 printers are not currently in circulation, they are for the experimental Ceramic resin use only.
After printing is complete the SLA parts go into a solvent bath to remove excess uncured liquid resin and then undergo a secondary UV light and heat cure process to reach their final material strength. Parts will continue to cure if exposed to UV light so a UV protectant coating is recommended for parts used as functional products. Due to the printing method resin printers always produce solid parts. This means the parts are water-tight, however they may absorb chemical solvents or interact chemically with castable resins. These parts typically require a support lattice in order to print successfully and remove from the build platform without failure. The support lattice may either be removed using wire snips or snapping them off by hand, depending on the resin. The material properties for the resins in stock at EPIC range from a soft flexible material to a rigid glass infused material. Formlabs provides ‘white papers’ on each material, including their material properties, on their website.
For resin prints please pay attention to the design constraints outlined by Formlabs in their Design Specs blog and SLA Tolerances (PDF). We will generally contact you regarding a print request if regions of your part seem too thin to print or holes seem too small. We cannot always tell if the resin will wash out of openings completely before they go into the post cure process.
Form3 printers can print handle up to 350mL volume parts depending on the geometry. If your part is too large for SLA, and cannot be traditionally fabricated, then FDM is a good option. If you are looking for transparent parts in the clear resin you can polish the finished print or spray coat it, visit Formlabs website for their detailed suggestions. Failures in resin parts usually occur when parts are too thin, when the tank ages, when parts are not supported well enough so they tear and stick to the bottom of the tank, or when parts warp during curing.
Queue Speed:
- We have 4 Form3 printers and 1 Form4 printer.
- Please submit one request per resin type.
- Each resin type requires its own tank, so we have one printer per resin. So your request cannot go on more than one printer at a time.
- Once a place in the queue is available most parts will take a day to print and if they are a small layer height (0.05mm, 0.025mm) they may take more than a day to print.
- Queue priority will be given based on our Policies and Prioritization page.
- You can check the status of your part, its place in the queue, and communicate with staff via our web portal located at bu.edu/epic/3d
Bambu Lab Printers
We also have 6 Bambu Lab X1C printers available in our First-In Cart for self-guided printing. Visit our page on the First-In cart for more information on using these printers.